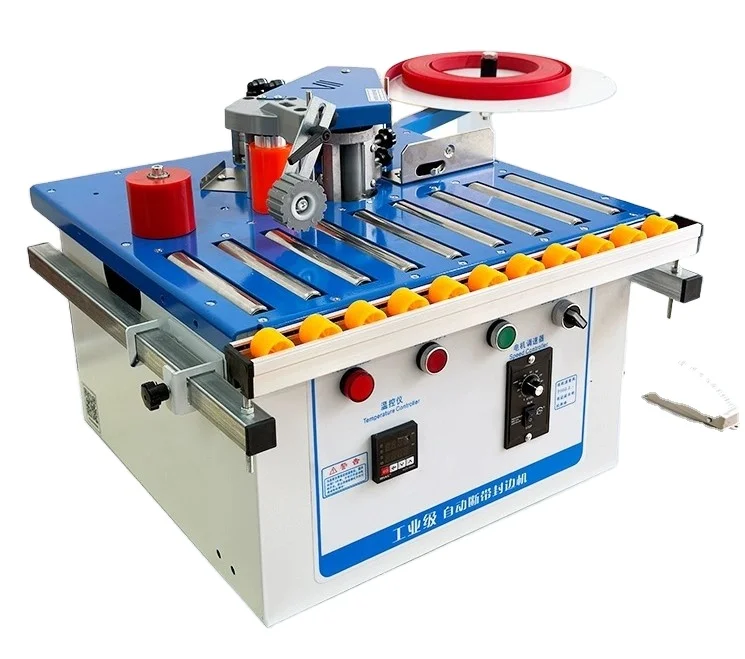
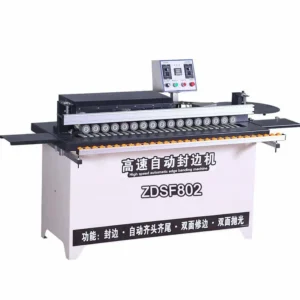
Voltage-First Configuration — The ZDSF50 is dispatched only after electrical schematics and local supply frequency are verified against the workshop's distribution panel, preventing the glue-pot underheating failures I have documented across Middle Eastern job sites.
Technical Specifications
| Parameter |
Value |
| Product Type |
Mini Portable Edge Banding Machine |
| Rated Power |
1.2 kW |
| Rated Voltage |
220V |
| Air Supply Requirement |
0.4–0.6 MPa |
| Feed Speed |
0–6 m/min |
| Edge Strip Thickness Range |
0.5–1.5 mm |
| Panel Thickness Range |
10–60 mm |
| Glue Pot Capacity |
1000 ml |
| Glue Heating System |
4 heating tubes |
| Heating Time |
5–10 min |
| Edge Strip Transport |
Adjustable bayonet according to edge strip height |
| Pressure Roller |
Adjustable, rubber material |
| Belt Breaking |
Pneumatic device with foot switch (curve) and travel switch (straight line automatic) |
| Function |
Double side gluing for straight, curved, and shaped edges |
| Overall Dimensions (L×W×H) |
54 × 54 × 56 cm |
| Net Weight |
26 kg |
| Warranty |
1 year |
Application Suitability
| Application |
Material or Output |
| Small joinery workshop production |
MDF, plywood, and particleboard panels with PVC edge banding |
| Custom furniture curved components |
Solid wood panels and shaped MDF with veneer or PVC strips |
| On-site installation adjustments |
Pre-cut cabinet doors and shelving requiring field edge finishing |
| Prototype and sample making |
Low-volume batch runs across mixed substrate materials |
Why the Voltage Question Should Come Before the Price on Mini Portable Edge Banding Machine Specifications
Confirming the local supply voltage and frequency against the machine's electrical schematic is the single most important step before any commercial discussion.
I have watched entire batches of cabinet doors get rejected because the glue pot could not maintain thermal stability on a mismatched supply. In one project, a 380V-rated heater element was fed from a 415V line, causing the thermal cutoff to trip repeatedly and leaving the adhesive below its activation temperature [NEED_CITE: voltage and frequency standards by export market]. The Mini Portable Edge Banding Machine specifications must be read against the workshop's actual distribution board, not against a catalog assumption. When the glue does not reach the correct viscosity, the edge strip appears bonded during inspection but delaminates within days of installation, creating warranty claims that cost far more than the machine itself.

Mapping Feed Speed to Small-Workshop Output
The ZDSF50 feeds material at 0–6 m/min, which positions it for workshops processing tens of panels per day rather than continuous production runs. At this speed range, the operator maintains visual control over the glue bead and strip alignment, reducing waste on expensive veneer materials. Matching the feed rate to the glue pot's 1000 ml capacity means the heater does not run dry during a typical batch, maintaining adhesive consistency from the first panel to the last.
Straight and Curved Edges in One Setup
The dual-mode belt-breaking system defines how this unit handles mixed geometry work. For straight edges, the travel switch triggers automatic strip cutoff once the panel passes the pressure zone, letting the operator focus on feed alignment. For curved and shaped profiles, the foot switch gives manual control over the cutoff point, which is necessary when the strip must follow a non-linear path without snapping or lifting at the radius [NEED_CITE: edge banding adhesion standards on curved substrates]. This eliminates the need for a second dedicated curved-edge machine in a space-constrained shop.
Reading the Specs That Affect Assembly Downstream
The panel thickness range of 10–60 mm and edge strip range of 0.5–1.5 mm define what this machine can physically process, but the downstream consequence matters more. A 1.5 mm PVC strip on a 60 mm particleboard shelf requires full glue penetration across the strip width; the four-tube heating system and double-sided gluing function address this by heating both the strip and the panel edge simultaneously. If the glue pot cannot sustain temperature at the upper thickness limit, the bond line remains visible and the panel fails visual QC. The adjustable pressure roller and transport bayonet must be set correctly for each thickness combination, or the strip will track off-center on thinner boards, producing an overhang that requires manual trimming and introduces inconsistency into the assembly stage.
What Happens When Configuration Is Skipped
Ordering a portable edge bander without verifying the air supply requirement against the shop's compressor leads to immediate operational failure. The pneumatic belt-breaking device requires 0.4–0.6 MPa to function; a compressor rated below this threshold will cause the cutoff mechanism to stall mid-cycle, leaving strip tails that damage the panel surface. Similarly, deploying this class of machine into a production volume it was never designed for — such as running eight-hour shifts on high-density MDF — accelerates wear on the rubber pressure roller and the transport bayonet beyond normal maintenance intervals [NEED_CITE: duty cycle expectations for portable woodworking equipment]. The result is unplanned downtime and strip adhesion failures that trace back to a specification mismatch, not a machine defect.
Why Source Through a Specification-Led Process
Every quotation for the ZDSF50 begins with a review of the buyer's electrical environment and panel processing requirements, not a generic price list. The manufacturer holds proprietary cutting mechanism patents and runs a four-stage QC protocol covering incoming material, in-process assembly, finished product testing, and pre-shipment verification. Voltage configuration from 110V to 440V is available as a standard option, and the control panel language is matched to the operator's working language before dispatch. An engineer-led configuration recommendation with a formal quotation is provided within 24 hours of receiving the buyer's technical brief, and factory visits are available for buyers who want to witness pre-shipment testing on their own panel stock.
Documentation & Verification
- CE declaration of conformity covering the ZDSF50 electrical and mechanical safety requirements
- Machine specification sheet with verified panel thickness and edge strip ranges
- Electrical schematic confirming rated voltage and heating circuit configuration
- Factory test record using buyer-supplied panel samples before dispatch
- Operation and maintenance manual translated into the agreed operator language
- Packing photographs and customs documentation support for export clearance
Installation, Commissioning & Support
- Requires a dedicated 220V circuit rated for the 1.2 kW load with proper earthing
- Compressor must deliver 0.4–0.6 MPa at the machine's pneumatic inlet before first run
- Arrives as a single 26 kg unit; position on a stable bench at operator waist height
- Glue pot heating system requires 5–10 minutes to stabilize before feeding the first panel
- Adjustable bayonet and pressure roller calibrated on-site to buyer's primary panel thickness
- Spare rubber pressure rollers and replacement heating tubes recommended for initial stock
Preparing Your Technical Inquiry
To receive an accurate configuration proposal, share the panel substrate types and thickness range your workshop processes most frequently, along with the edge strip material and width you intend to use. Include a photograph of your distribution board nameplate so the voltage and frequency can be confirmed before the electrical schematic is finalized. If your production includes curved or shaped panels, specify the minimum radius and the strip thickness required at those profiles so the pneumatic cutoff system is set correctly before dispatch.
Frequently Asked Questions
Q: How do I verify the ZDSF50's feed speed and glue capacity against my daily panel output?
A: Calculate your typical daily linear meters of edge to be banded and compare against the 0–6 m/min feed speed, factoring in loading and unloading time between panels. The 1000 ml glue pot sustains continuous operation for a defined period depending on strip width and glue application rate. For higher volumes, confirm with the engineering team whether this model's duty cycle matches your shift pattern.
Q: Does the 220V rating match my local voltage, and can the machine be configured for other standards?
A: The standard rating is 220V, but voltage configuration from 110V to 440V is available as a factory option. Share your distribution board nameplate photograph so the engineering team can confirm the correct heater element and motor winding specification before production. This prevents the glue-pot underheating failures that occur when voltage is assumed rather than verified.
Q: What panel and edge strip thickness combinations are supported, and where are the limits?
A: The machine handles panels from 10 to 60 mm thick and edge strips from 0.5 to 1.5 mm. At the upper limits — such as 1.5 mm PVC on 60 mm particleboard — the four-tube heating system must maintain full temperature across the bond surface. Confirm your specific material combination with the engineering team to verify that the pressure roller and transport bayonet are pre-set for your primary workload.
Q: How does the dual belt-breaking system affect operator workflow on curved versus straight edges?
A: Straight edges use the travel switch for automatic strip cutoff, allowing the operator to focus on feed alignment and speed. Curved and shaped edges use the foot switch for manual cutoff timing, which is necessary when the strip follows a non-linear path. This dual-mode design means one operator can handle mixed-geometry batches without changing tooling or switching machines.