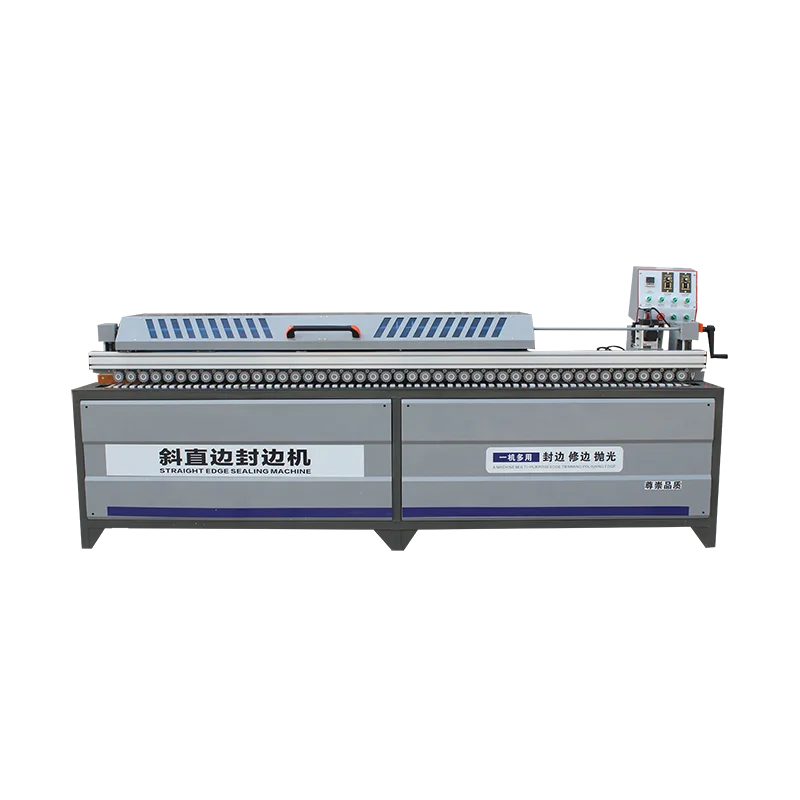
Engineer-Led Configuration — Every ZDSDW3000 quotation includes confirmed voltage, panel thickness compatibility, and substrate-specific feed parameters before production begins.
Technical Specifications
| Parameter |
Value |
| Model |
ZDSDW3000 |
| Product Type |
Oblique Straight Edge Banding Machine |
| Function Stations |
Gluing, Fine Trimming, Rough Trimming, End Trimming, Scraping, Buffing |
| Pre-milling |
Included, upstream of gluing station |
| Bevel Pressing |
8 groups, adjustable 30° to 90° |
| Pressure Beam Adjustment |
Digital display height setting |
| Gluing Device |
Integrated, ensures tight edge band to board contact |
| Polishing |
Dual motors, upper and lower |
| Dust Extraction |
Large-diameter suction tube |
| Overall Dimensions (L×W×H) |
2990 × 650 × 1300 mm |
| Rated Power |
To be confirmed at quotation |
| Voltage & Frequency |
Configurable 110V–440V, confirm local supply |
| Feed Speed |
To be confirmed based on substrate and panel mix |
| Panel Thickness Range |
To be confirmed per configuration |
| Tolerance |
To be verified during factory test on buyer's substrate |
| Control System |
Confirm PLC / relay / inverter configuration at inquiry |
Application Suitability
| Application |
Material or Output |
| Custom cabinet door edge finishing |
MDF and plywood with PVC or veneer banding |
| Wardrobe and shelving panel edging |
Particleboard with melamine or ABS edge band |
| Oblique profile furniture components |
Solid wood panels requiring 30°–90° bevel edge finish |
| Retail fixture and shopfitting panels |
Mixed substrate runs with frequent thickness changes |
| Joinery workshop short-run production |
Small batches on plywood, MDF, and blockboard |
What "Standard Voltage" Leaves Out When Ordering an Oblique Straight Edge Banding Machine
Assuming a default electrical configuration is the most common reason edge banders arrive on site and cannot be powered up.
I spent years on the assembly floor before moving into machine configuration for buyers. One pattern keeps repeating: a buyer receives a quotation with a price and a model number, but the voltage and frequency were never matched to the local grid. The machine lands at the workshop, the electrician opens the panel, and the inverter is rated for 380V 50Hz while the facility runs on 220V 60Hz. Commissioning stalls before the first panel is fed [NEED_CITE: voltage and frequency standards by export market]. When selecting a ZDSDW3000 oblique straight edge banding machine, the electrical schematic and voltage confirmation must be settled before the order enters production.

Eight-Group Bevel Pressing and Why Adjustability Matters
The ZDSDW3000 carries eight pressing groups with angles adjustable from 30 to 90 degrees. This range covers both standard straight-edge work and oblique profiles common in contemporary cabinet and furniture design. Each pressing group applies consistent contact pressure along the band-to-panel joint, which is critical when switching between thin PVC and thicker veneer materials within the same production shift.
Digital Pressure Beam Height and Panel Thickness Matching
The digital display for pressure beam height adjustment removes the trial-and-error step that slows down changeovers. When a workshop runs 16 mm particleboard in the morning and 25 mm MDF in the afternoon, the operator sets the beam height from the display rather than adjusting by hand and test-feeding scrap pieces. This specification directly affects edge banding consistency across a mixed-substrate schedule and is worth confirming against the actual panel thickness range you plan to process [NEED_CITE: CE machinery directive requirements for panel processing equipment].
Pre-Milling, Trimming Stations, and Downstream Assembly Quality
The pre-milling motor upstream of the gluing station squares the panel edge before adhesive application. On particleboard with uneven saw cuts, this step removes the fractured fiber layer and creates a flat bonding surface. Downstream, the six trimming stations — gluing, fine trimming, rough trimming, end trimming, scraping, and buffing — each address a specific stage of edge finish. The tolerance you achieve at the trimming stage determines whether panels assemble flush in the carcass or show visible step-offs at the joints. When evaluating ZDSDW3000 edge banding machine specifications, ask for a factory test record on your own substrate to verify the actual finish rather than relying on catalog claims.
The Cost of Skipping Substrate-Specific Feed Testing
A configuration that runs flawlessly on medium-density MDF may stall or chip edge banding on high-density particleboard at the same feed speed. I have seen workshops purchase an edge bander rated for a certain throughput, only to discover that their specific board stock forces the feed rate down to maintain acceptable edge quality. The result is actual output well below the quoted figure. Before committing to any oblique straight edge banding machine, request a sample processing test using the exact substrate density and edge band material you run daily [NEED_CITE: substrate density impact on edge banding feed speed].
Why Procurement Verification Starts Here
The ZDSDW3000 is built on an in-house manufacturing process with patented cutting mechanisms and verified tolerance checkpoints. Every unit passes through four-stage quality control covering incoming material, in-process inspection, finished product review, and pre-shipment verification. Voltage, control language, and specification customization are handled as standard steps in the quotation, not as afterthoughts. The full product family — from entry-level to full-function pre-milling configurations — means a workshop can scale its edge banding capacity without switching suppliers. Each machine ships with an operation manual in the agreed language, matched electrical documentation, and a factory test record specific to the buyer's panel mix.
Documentation & Verification
- Machine specification sheet confirming all station functions and dimensional data
- Electrical schematic with voltage and frequency matched to your facility supply
- Factory test record using your panel thickness range and edge band material
- Operation and maintenance manual in the agreed operator language
- Pre-shipment verification photographs documenting edge finish quality
- Customs documentation support for destination-country import requirements
Installation, Commissioning & Support
- Confirm dedicated circuit capacity matching the ZDSDW3000 rated power before delivery
- Verify workshop floor levelness across the 2990 mm machine length for stable panel feeding
- Set pressure beam digital display to your most common panel thickness at first startup
- Configure bevel pressing groups to your primary angle range before the first production run
- Establish dust extraction ductwork diameter to match the large-diameter suction port
- Schedule initial feed speed calibration on your actual substrate mix with technician guidance
Preparing Your Inquiry
Share your primary panel materials, thickness range, and the edge band types you use most frequently. Include your local voltage and frequency so the electrical configuration is confirmed before production. If you run oblique profiles, specify the bevel angles required so the pressing groups are preset at the factory.
Frequently Asked Questions
Q: What panel thickness range and feed speed does the ZDSDW3000 support?
A: The panel thickness range and feed speed depend on the specific configuration and your substrate density. Request a machine specification sheet with confirmed figures matched to your board stock. A factory test on your actual material verifies both parameters before you commit to an order.
Q: How is voltage confirmed before the machine ships?
A: Your local voltage and frequency are documented in the electrical schematic during the quotation stage. The control panel, motors, and inverter are configured to match. A voltage confirmation document is included in the shipping documentation package.
Q: What trimming tolerance can I expect on my panels?
A: Tolerance is verified during a factory test using your substrate and edge band material. The pre-milling station and six trimming functions work together to produce the final edge quality. Request the test record with measured results before shipment.
Q: Which stations are essential versus optional for my application?
A: Pre-milling and bevel pressing are essential for panel edge flatness and oblique profile work. Polishing and scraping determine final surface finish. Your substrate mix and quality standard determine which stations your production requires.
Q: How should I plan dust extraction and air supply for this machine?
A: The ZDSDW3000 uses a large-diameter suction tube for dust collection. Confirm the duct diameter and airflow requirement against your workshop's existing extraction system. Air supply specifications are included in the machine documentation for your facility planning.