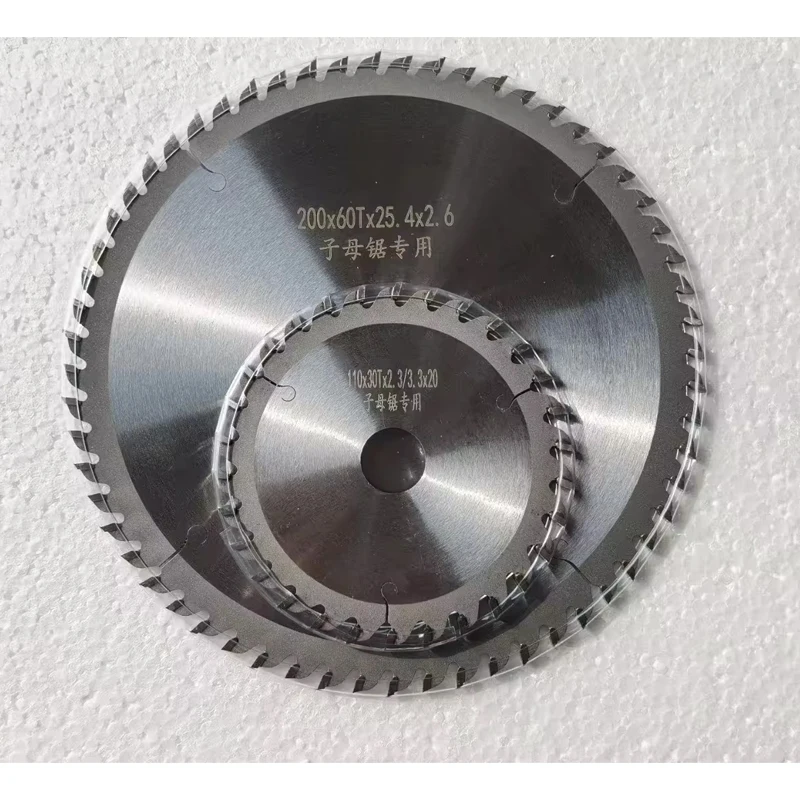
Precision Ground Blade Interface — Every Dust Free Mother Saw Blade leaves the factory with verified arbor fit and tooth geometry checked against the declared panel substrate, so the cut edge matches the tolerance your assembly line demands.
Technical Specifications
| Parameter |
Value |
| Product Type |
Dust Free Mother Saw Blade |
| Blade Application |
Panel cutting and sizing on sliding table saws and panel saws |
| Compatible Substrates |
MDF, particleboard, plywood, solid wood panels |
| Dust Extraction Integration |
Designed for connection to standard workshop extraction systems |
| Cutting Action |
Main scoring and sizing cuts with minimized airborne particulate |
| Edge Finish Target |
Clean cut edges reducing post-processing on visible panel surfaces |
| Machine Compatibility |
Sliding table saws and panel saws with standard arbor configurations |
Application Suitability
| Application |
Material or Output |
| Custom cabinet panel sizing |
MDF and melamine-faced particleboard |
| Wardrobe and shelving board cutting |
Plywood and veneered board |
| Furniture component dimensioning |
Solid wood panels and engineered board |
| Clean-room or low-dust workshop cutting |
All common panel substrates where dust control is specified |
Why the Spec Sheet Matters Before You Order the Blade
A blade that does not match your saw's arbor, feed speed, and substrate will produce chipped edges regardless of how sharp it arrives.
I have walked into workshops where the operator blamed the saw for tear-out on melamine particleboard, only to find the blade tooth geometry was meant for solid wood ripping. The Dust Free Mother Saw Blade specifications need to be checked against the actual panel material and the feed rate your operators use daily. When the tooth count, hook angle, and plate thickness are not confirmed before the order, the blade may cut cleanly on the first sheet but degrade quickly once production volume picks up [NEED_CITE: cutting tool selection standards for engineered wood panels].

How Dust Extraction Geometry Affects Your Workshop Air
The tooth gullet design and plate body on a dust-free blade are shaped to direct chips and fine particulate toward the extraction port rather than letting them scatter across the table. On MDF and fine particleboard, the dust fraction is significant, and airborne particles settle on glue pots, edge bander beds, and bore heads downstream. Keeping that particulate out of the air means less cleaning between jobs and more consistent adhesive bonding on subsequent operations. The Dust Free Mother Saw Blade specifications should be read alongside your extraction system's airflow rating to confirm the blade and ductwork are matched.
Substrate-Specific Tooth Selection for Panel Plants
Different engineered boards demand different cutting approaches. Particleboard with a coarse core chips easily on the exit side if the tooth hook angle is too aggressive. Plywood with alternating grain directions needs a tooth geometry that shears rather than lifts. MDF produces the finest dust of all common panel materials, making extraction geometry as important as edge sharpness. Selecting the correct blade variant for your primary substrate prevents the situation where a blade performs well on one board type but tears out on another [NEED_CITE: substrate-specific saw blade selection in furniture manufacturing].
Reading the Numbers That Actually Matter
Arbor diameter determines whether the blade physically fits your saw spindle — a mismatch means the blade cannot be mounted at all. Blade diameter sets the maximum cutting depth, which directly limits the panel thickness you can size in a single pass. Tooth count influences both cut quality and feed speed: higher tooth counts produce cleaner edges on melamine and veneered surfaces but require slower feed rates to avoid burning. Plate thickness affects kerf width and the power demand on your saw motor. These four parameters together define whether the blade will work in your specific saw and on your specific panel mix.
The Cost of Guessing the Wrong Blade Configuration
When a blade is ordered without confirming arbor size, it arrives and sits on a shelf until an adapter or replacement saw is sourced. When tooth geometry is wrong for the substrate, operators slow the feed rate to compensate, cutting throughput and pushing delivery dates back. Chipped edges on visible cabinet panels mean re-cuts, wasted board, and delayed assembly. In a multi-machine workshop, running the wrong blade on one saw creates a bottleneck that affects the entire cutting schedule [NEED_CITE: hidden costs of incorrect tooling in panel processing].
Why Procurement Starts with Verification Here
In-house manufacturing means blade plate grinding and tooth brazing are controlled under one roof, not outsourced in stages. Four-stage quality control covers incoming carbide, in-process brazing inspection, finished runout checks, and pre-shipment verification before the blade leaves the factory. Voltage confirmation on the saw motor is standard in the configuration conversation, because a blade is only as good as the saw driving it. Engineer-led configuration means the recommendation is based on your panel types and saw models, not a catalogue page. Factory test records on your specified materials are available before dispatch.
Documentation & Verification
- Machine specification sheet confirming arbor diameter and blade diameter match to your saw model
- Factory test record showing cut edge quality on your declared panel substrates
- Electrical schematic and voltage confirmation for the host saw system
- Operation and maintenance manual covering blade mounting, alignment, and replacement intervals
- Spare parts list for matching scoring blades and wear components
Installation, Commissioning & Support
- Verify arbor diameter and flange condition on your sliding table saw before mounting the blade
- Confirm saw motor voltage and frequency match local supply to prevent underpowered cuts
- Align the blade to the fence and sliding carriage using the saw's built-in adjustment mechanism
- Run test cuts on your actual MDF or particleboard stock and adjust feed speed accordingly
- Schedule regular tooth inspection based on panel volume to maintain edge quality
What to Send With Your Inquiry
Provide the make and model of the sliding table saw or panel saw the blade will mount on, along with the primary panel substrates you cut and their typical thickness range. Share your local voltage and frequency so the host machine specification can be confirmed at the same time. If you run multiple board types across shifts, list them in order of volume so the tooth configuration can be matched to your heaviest workload.
Frequently Asked Questions
Q: How do I confirm the blade will actually reduce dust in my workshop?
A: Dust extraction performance depends on the blade geometry working together with your extraction system's airflow capacity. Request a factory test record on your specific panel material and compare the dust capture result against your workshop's extraction specifications. The blade directs particulate toward the port, but the ductwork and fan must be sized to handle the volume generated at your operating feed speed.
Q: What blade specifications should I match to my panel thickness and feed speed?
A: Blade diameter must allow sufficient cutting depth for your thickest panel. Tooth count should be selected based on your primary substrate — higher counts for melamine and veneered boards at moderate feed speeds, lower counts for rapid sizing of raw particleboard. Confirm the arbor diameter against your saw spindle before ordering to avoid fitment issues on arrival.
Q: Will this blade fit my existing sliding table saw or panel saw?
A: Fitment depends on three dimensions: arbor diameter, blade diameter, and plate thickness relative to your saw's flange and guard clearance. Provide your saw make and model so these can be cross-checked before production. Adapters are available for some arbor mismatches, but they add runout risk and are not recommended for precision panel cutting.
Q: How often should I inspect or replace the blade to maintain cut quality?
A: Inspection intervals depend on panel volume, substrate abrasiveness, and feed speed. MDF and high-density particleboard wear carbide teeth faster than plywood or solid wood. Check tooth edges and runout at regular intervals based on your shift volume and replace or resharpen when edge chipping appears on the exit side of the cut or when feed resistance increases noticeably.